Mitsubishi Electric Automation Systems Division UK is urging manufacturers to identify and reduce wasted energy within existing production facilities as industrial electricity costs continue to influence competitiveness. The company argues that plant operators can exercise more direct control over consumption, equipment loading and production processes than over volatile wholesale prices.
The recommendation comes as the British Industrial Competitiveness Scheme, or BICS, progresses towards support for eligible manufacturing businesses from April 2027. Applications for its first year are open until 30 November 2026. Although the scheme is intended to reduce the indirect policy costs included in eligible electricity bills, it does not replace the operational case for reducing energy consumption per unit of production.
European manufacturers continue to face a material energy price disadvantage relative to US competitors. The European Union Agency for the Cooperation of Energy Regulators, ACER, found that EU gas and electricity prices remained structurally higher than those in the United States in its 2026 monitoring report. That analysis primarily covers 2025 market data; historical cross-market ratios should not be interpreted as live November 2026 quotations or as the tariff faced by every factory.
David Bean, Business Development Group Manager at Mitsubishi Electric Automation Systems Division, said manufacturers had traditionally concentrated their energy strategies on prices. Before successive energy price shocks, he suggested, relatively stable energy costs made production inefficiencies easier to absorb. The volatility of subsequent years has increased the value of controlling consumption within the factory, regardless of the wholesale tariff.
Rising costs can expose waste that was previously hidden in overhead expenditure. A machine may consume substantial electrical power while waiting for the next component, a compressed air system may maintain pressure despite low production demand, and a process may be run at a fixed setting even when the required output has fallen. These conditions differ operationally, so the remedy has to follow measured consumption rather than a single factory-wide target.
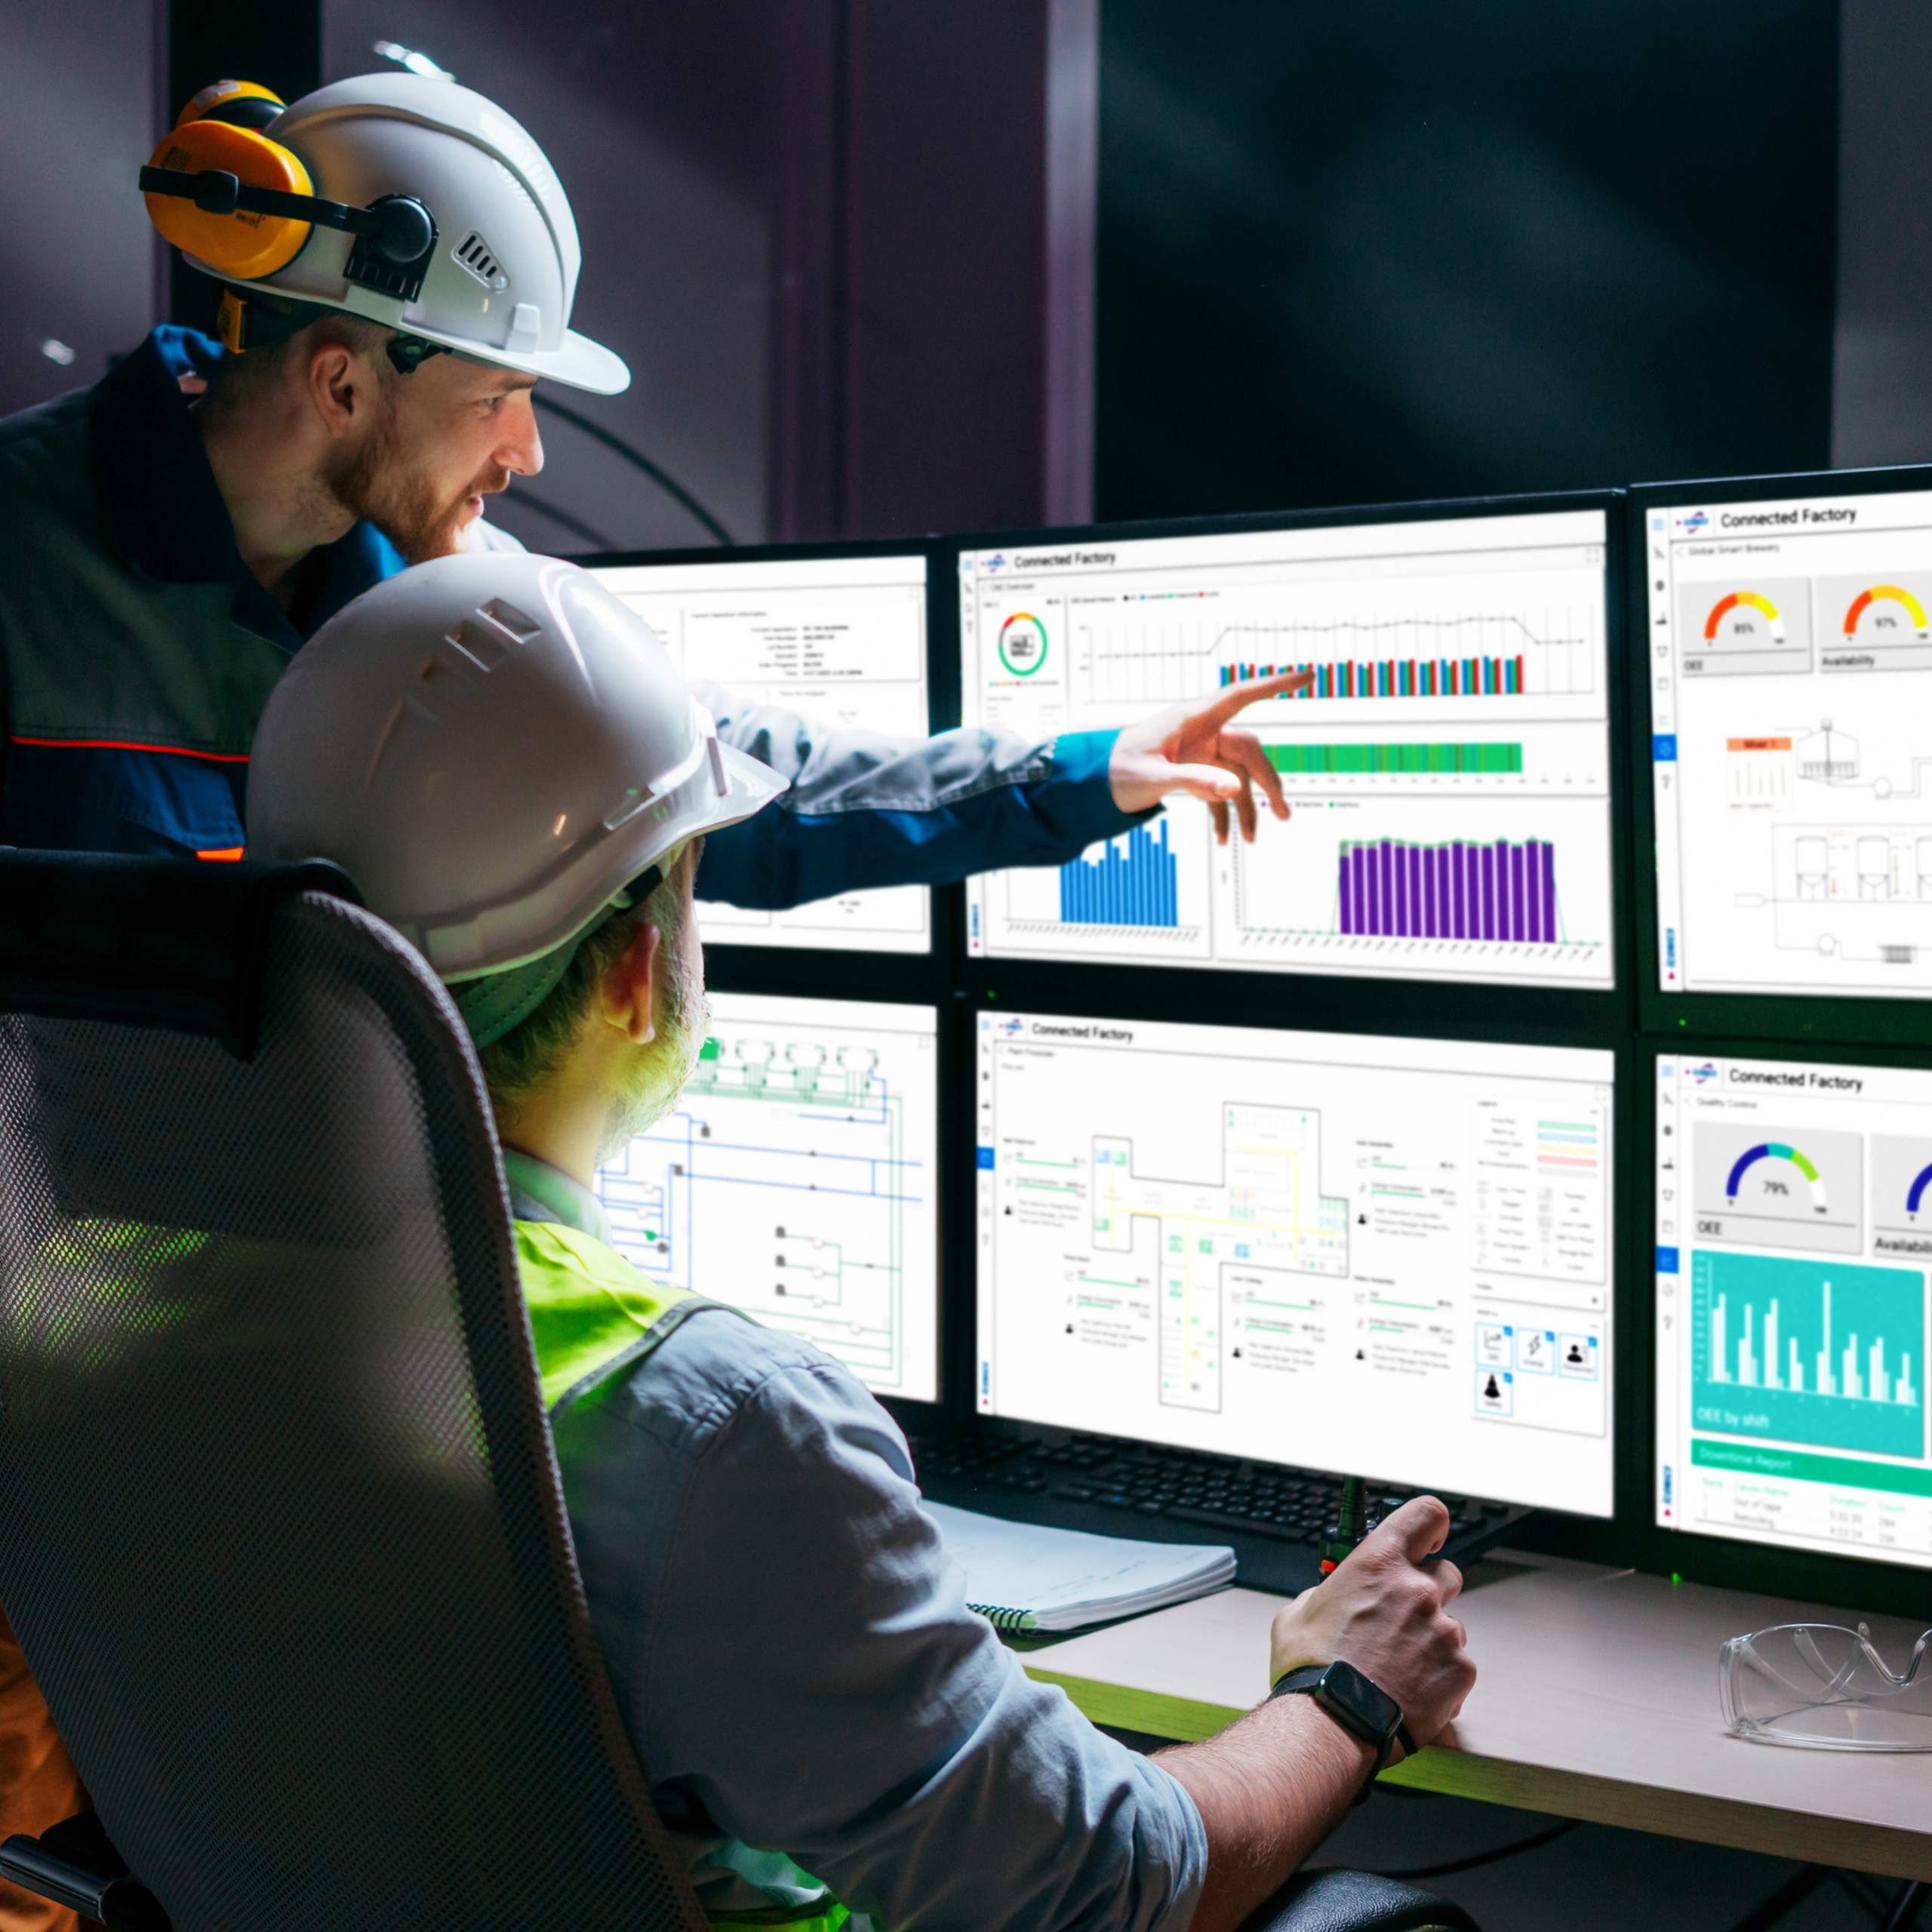
Bean said the more useful starting point is to examine energy use across production lines, identify the most intensive processes and determine where automation can improve consumption. In practice, that requires energy readings to be associated with production states, batch information, equipment availability and output. A total monthly electricity bill cannot establish whether a particular line is efficient because it conceals variations in product mix, operating time and utilisation.
Submetering and equipment-level data can distinguish the energy consumed during production from that drawn during idle or standby periods. When consumption is compared with units produced or an appropriate physical process measure, engineers can establish an energy baseline and investigate departures from expected performance. Comparisons have to account for differences in product specifications, material condition, ambient conditions and shifts rather than treating every operating hour as equivalent.
Automation systems provide possible corrective mechanisms once the sources of waste are understood. Variable-speed drives can reduce the output of motors where a process genuinely allows speed adjustment; scheduling systems can coordinate start-up and standby periods; and control logic can reduce unnecessary running of ancillary equipment. Such changes require checks on production quality, throughput, reliability and safety before energy savings are regarded as operational gains.
Compressed air, pumping, ventilation, refrigeration and heating systems can warrant particular attention because utility equipment frequently continues operating outside active production periods. A pressure setpoint that is higher than the process requires can increase compressor demand, while poorly coordinated pump or fan controls can waste energy. Maintenance faults, leaks and worn components can also change consumption profiles without producing an obvious immediate failure.
Efficiency programmes need to avoid reducing electricity use by simply slowing a line or shifting work elsewhere. A decrease in total consumption alongside a larger fall in output may raise the energy consumed per finished unit. The same issue arises when a machine is switched off during a shift but production is transferred to a less efficient process, or when additional scrap eliminates the expected benefit of a lower power setting.
Properly measured improvements allow businesses to distinguish cost reduction from changes in production volume. Reliable baselines can also support investment decisions by comparing the cost of instrumentation, control changes and maintenance against achievable savings. A useful project should identify the conditions in which the improvement holds, the risks of changing process parameters and the method used to verify results after implementation.
The BICS scheme addresses eligible electricity costs through a separate policy mechanism. The manufacturer’s site and business activities must meet the stated qualification rules, and businesses should not assume that every factory will benefit. Support beginning in April 2027 will also not remove exposure to changes in consumption, contract terms or other energy charges.
Bean identified production lines and energy intensive processes as starting points for action. He said: “This means examining how much energy is being wasted across their production lines, which processes have the highest energy intensity, and where automation can help to optimise consumption.” The approach requires energy and output data to be compared against an agreed operating baseline before interventions can be evaluated.
Applications for the first year of BICS close on 30 November 2026, and support for qualifying manufacturing sites is due from April 2027. At plant level, the relevant measure of efficiency remains energy consumed per unit of conforming output, assessed alongside throughput, safety, equipment reliability and product quality. Those operating measurements can continue irrespective of which electricity cost relief a site ultimately receives.