Ball Corporation plans to establish a new aluminium beverage can manufacturing plant in Baruth, Germany, expanding its European production network to support long-term demand from an existing energy drinks customer.
The investment was confirmed on 3 November alongside Ball’s third-quarter financial results. The proposed facility will contain multiple production lines, with manufacturing ramp-up expected to begin in late 2028.
Ball has not disclosed the capital investment value, the number of production lines, the plant’s intended annual capacity or the identity of the customer supporting the project.
Chief executive Ron Lewis described the development as an investment linked to a long-term commercial relationship with a customer seeking additional production capacity for its European business.
The project is intended to strengthen Ball’s existing manufacturing network in Europe, the Middle East and Africa (EMEA), where the company reported higher packaging shipments during the third quarter.
Ball’s global aluminium packaging shipment volumes increased 4.7% year on year. Its EMEA packaging segment recorded mid-single-digit percentage volume growth, accompanied by higher sales and comparable operating earnings.
The EMEA segment reported third-quarter sales of approximately $1.33 billion, compared with $1.13 billion in the corresponding period of 2025. Comparable operating earnings increased from $164 million to $170 million.
These results cover the company’s wider regional operations, including changes to its business structure. They do not establish a specific rate of demand growth in Germany or quantify the volume expected to be manufactured at Baruth.
The company’s EMEA results include its acquisition of an 80% interest in Benepack’s European beverage can manufacturing business in January 2026. That transaction added manufacturing facilities in Belgium and Hungary, while Ball’s new Baruth project represents a separate investment in production capacity.
The German factory is being developed around a long-term customer requirement rather than a general forecast of growth across the entire national beverage packaging market.
Lewis said: “We invest when our customers ask us to invest on their behalf for their growth”.
The company uses long-term customer agreements to support decisions about major capital investments, helping establish expected demand before committing to new production equipment.
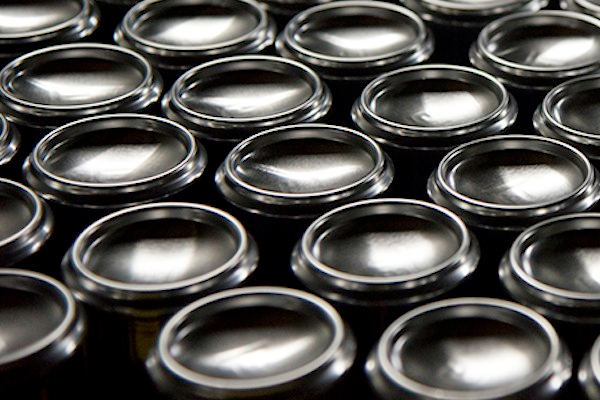
An aluminium beverage can factory requires substantial manufacturing infrastructure. High-volume production involves equipment for forming containers from metal sheet, finishing their surfaces, applying coatings and decoration, and inspecting the completed products.
In the widely used drawn and wall-ironed manufacturing process, aluminium sheet is supplied in coils and fed into equipment that forms shallow cups. These are subsequently drawn and ironed to create the can body, reducing wall thickness while maintaining the required dimensions.
The process depends on the characteristics of the incoming metal, the condition of the forming equipment and the control of operating parameters.
Aluminium alloys and sheet specifications are selected to provide appropriate forming performance and the mechanical characteristics required by the finished container. Variations in material properties can influence how the sheet behaves during the drawing and ironing operations.
Tooling condition and process settings also affect the geometry and surface characteristics of can bodies. Manufacturing defects can result in rejected products or require corrective changes to the equipment.
After forming, can bodies undergo further processing. Depending on the product, operations can include washing, surface treatment, coating, printing, curing, neck forming and preparation for packing or shipment.
Internal coatings are selected to suit the intended beverage and its storage conditions. They provide a barrier between the contents and the metal container, with suitability dependent on the coating formulation, application and curing process.
External printing and finishing allow customers to specify the required decoration and product appearance. The manufacturing line must maintain print and coating quality while operating at the throughput needed for commercial supply.
The dimensions of the finished can also matter. Body geometry and neck dimensions must be compatible with the appropriate closure system and the customer’s filling equipment.
A container produced outside the agreed dimensional tolerances may create difficulties during handling, filling or sealing. Inspection is therefore incorporated into industrial can manufacturing to identify defects and confirm that products meet the required specifications.
Automated systems can examine dimensional and surface characteristics at different points in production. Their configuration depends on the equipment and the defects that must be detected.
High-volume production also requires supporting systems for moving aluminium coils, handling finished products and collecting manufacturing scrap. Waste generated during forming and trimming can be recovered for recycling, subject to appropriate material handling arrangements.
The ability to reuse aluminium is a significant characteristic of the material, but the environmental performance of a completed packaging system depends on several factors, including material sourcing, production energy and the proportion recovered after use.
Ball has not published the equipment specification for the proposed Baruth factory, so its intended forming technology, line speeds and material handling arrangements remain to be confirmed.
Those details will influence the plant’s eventual output and the range of packaging formats it can manufacture. A multi-line configuration allows production to be distributed between lines, although the operating capabilities will depend on the machinery selected.
Factory development also requires suitable utility connections, production buildings, storage space and transport infrastructure. The installation and commissioning of manufacturing equipment must be coordinated with those supporting systems.
When a new production line begins operating, manufacturers need to establish that the equipment can produce containers meeting customer requirements consistently. This normally involves trials, quality checks and the progressive adjustment of operating conditions.
Late 2028 is the target for the beginning of the Baruth ramp-up, rather than a confirmed date at which the facility will operate at full capacity.
Ball has not disclosed a detailed construction programme, employment target or subsequent capacity milestone. The timing of equipment installation and qualification will become clearer as the project progresses.
The investment forms part of a wider programme to expand the company’s international beverage packaging operations.
In September, Ball announced plans for a two-line manufacturing facility in Uttar Pradesh, India. The Indian plant is expected to begin operating in 2029 and will complement the company’s established facilities at Taloja and Sri City.
The Indian and German projects are intended to serve different regional markets, with their development supported by customer requirements and separate commercial arrangements.
For Ball, the decision to add production capacity follows a period of higher global shipment volumes. The company has identified energy drinks and non-alcoholic beverages among the categories supporting demand for aluminium packaging.
The scale and location of new production investments depend on the volumes required by individual customers, the products being supplied and the economics of operating the associated manufacturing equipment.
Material and energy costs also influence those economics. Aluminium is a substantial production input, while forming, washing, coating and curing equipment require power and supporting utilities.
Ball’s third-quarter financial performance reflected both higher packaging shipments and changes in selling prices and material costs.
At group level, quarterly revenue increased to approximately $4.19 billion from $3.38 billion a year earlier. Comparable operating earnings rose to $451 million from $440 million.
The company recorded a statutory net loss attributable to shareholders of $94 million, compared with net earnings of $321 million in the third quarter of 2025.
These statutory results differ from Ball’s comparable earnings measures, which exclude certain specified items. The figures describe overall financial performance rather than the projected profitability of the German factory.
Ball expects continued demand growth and is directing new capacity towards projects supported by long-term customer commitments. The Baruth investment is one of the developments intended to accommodate that growth beyond the company’s existing manufacturing network.
The next project milestones will involve construction planning, equipment procurement and preparation for manufacturing. Ball’s target remains to begin production ramp-up in late 2028, with the factory’s eventual output dependent on the completed line configuration and successful qualification of the cans manufactured for its customer.