PackworldUSA has detailed how resistance-based temperature control is used in impulse heat sealers for medical, pharmaceutical and wider industrial packaging. Its technical article, dated 19 October, covers machines incorporating control technology supplied by TOSS Machine Components. The heating band acts as both the source of heat and the feedback element, allowing the controller to adjust electrical input during each short sealing cycle. This is an examination of established equipment rather than the launch of a new sealer.
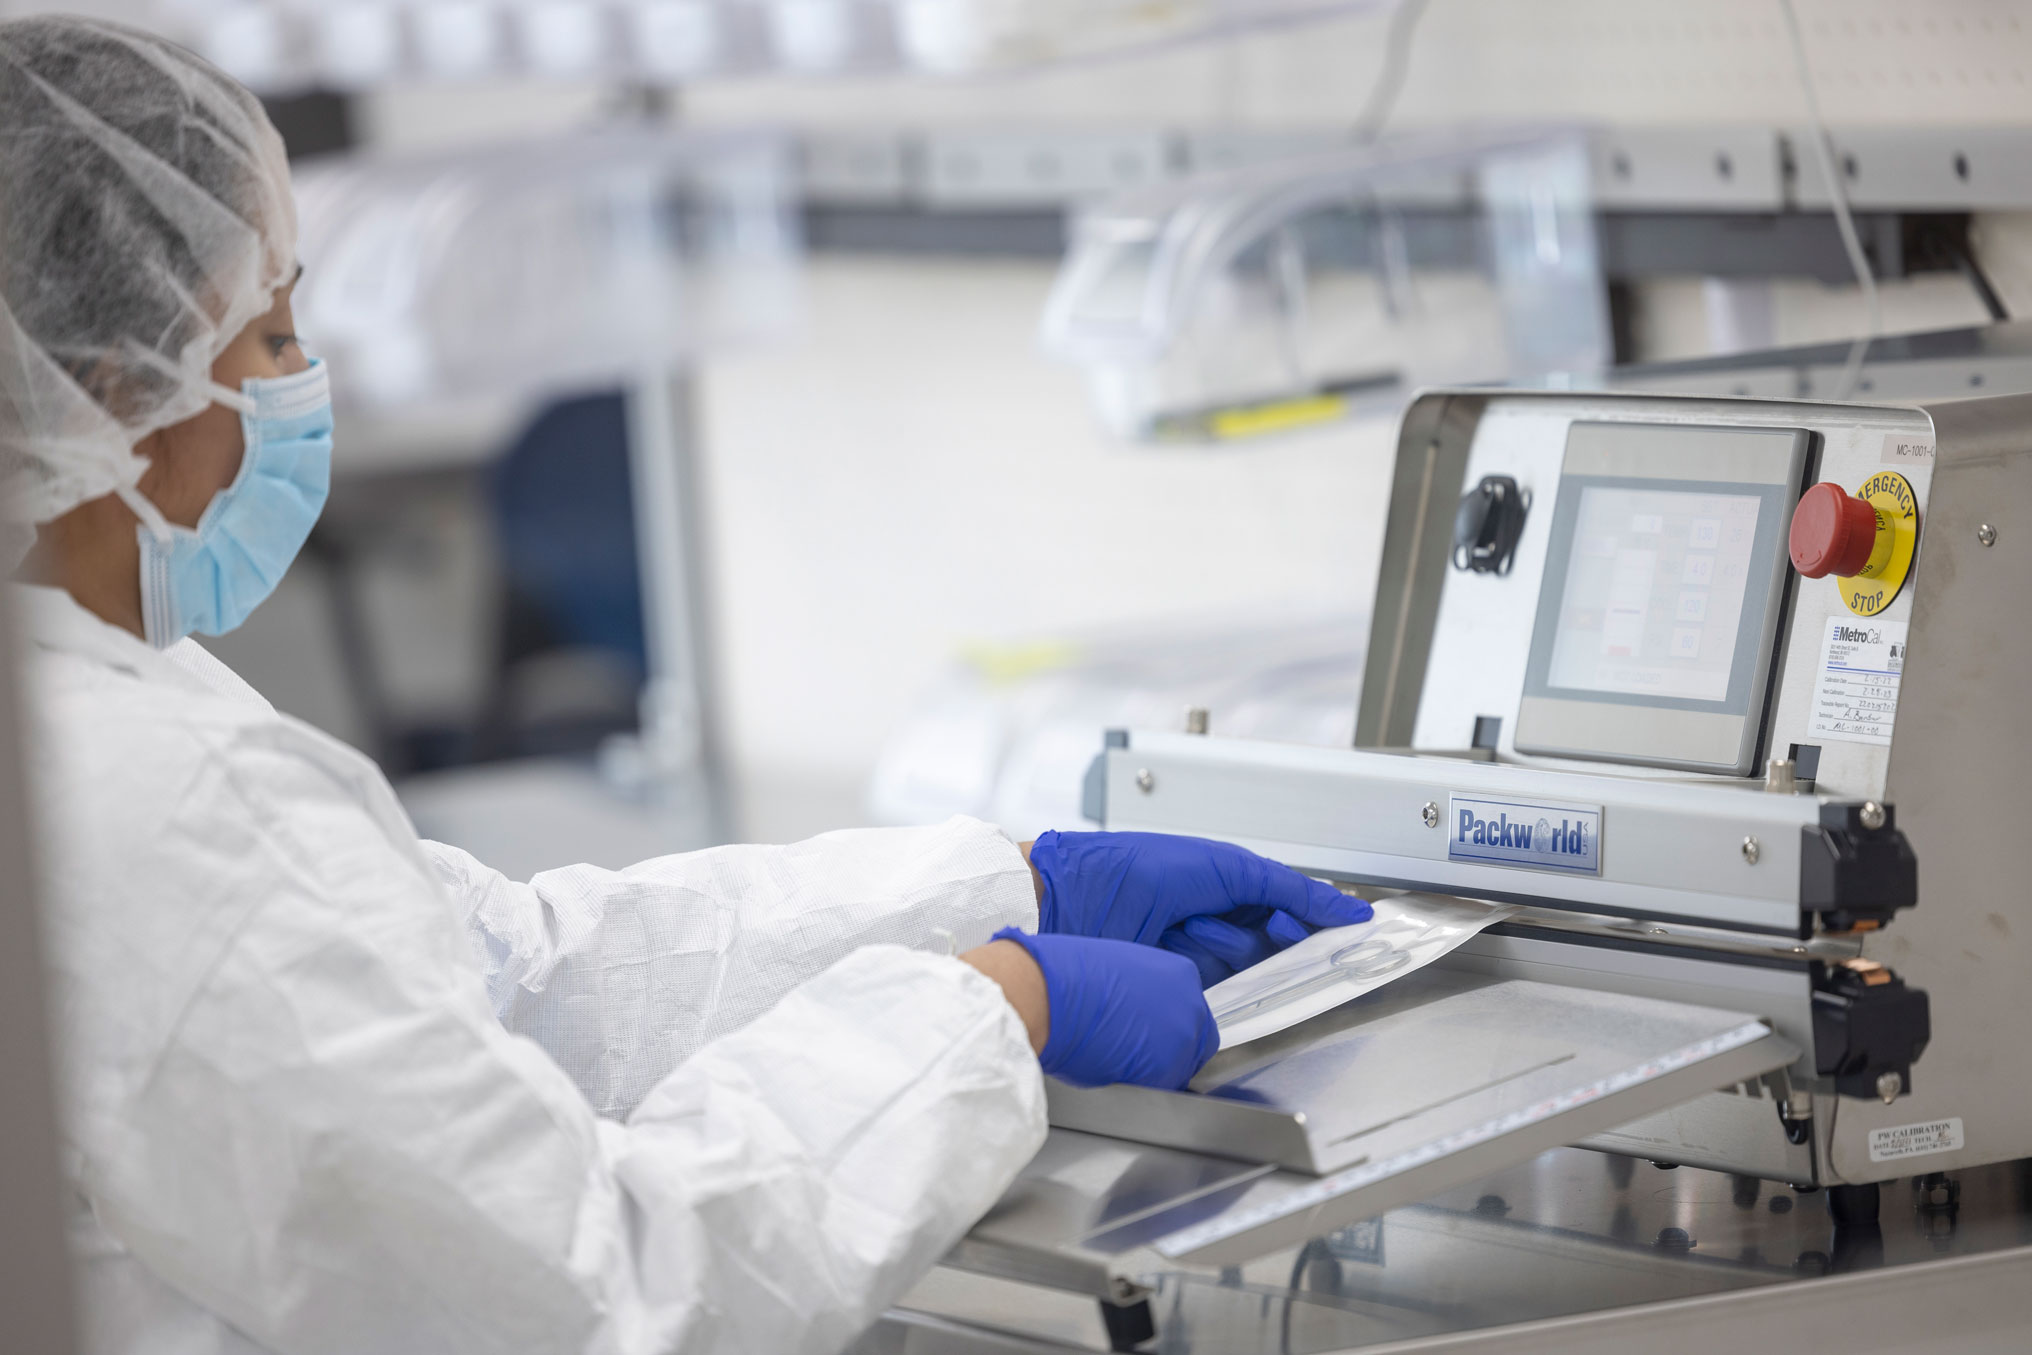
An impulse sealer holds compatible thermoplastic surfaces between jaws, passes current through a heating element and allows the joint to cool before releasing the material. Heat must reach the interface at a suitable rate, remain within the material’s joining window for long enough, and then dissipate while the package is still supported. A continuously heated bar keeps its tool hot between cycles; impulse equipment applies power for a defined portion of the cycle. Neither method guarantees a sound seal without appropriate pressure, film properties and contact conditions.
TOSS Variable Resistance Control, or VRC, uses the change in electrical resistance of its specified sealing alloy as the temperature-dependent feedback signal. Its PIREG controller reads heating-element voltage and current, calculates resistance and compares the result with the calibrated relationship between resistance and temperature. The controller then regulates the electrical heating input. This eliminates the need to rely on a separately mounted thermocouple as the normal feedback sensor during each impulse, although external instruments may still be needed for calibration, process qualification or independent verification.
A contact thermocouple reads temperature where its junction is installed, which can create lag or positioning uncertainty during rapid thermal changes. Measuring resistance across the heated circuit instead responds to the electrical state of the band itself. The result is not a map of seal-interface temperature at every point along the jaws: a contaminated section, uneven jaw pressure or a locally damaged element can create variation that a whole-element measurement does not separately resolve. Mechanical inspection and seal testing therefore remain necessary.
TOSS pairs its PIREG controls with Alloy-20 sealing bands in straight, shaped and other configurations. Element geometry governs the current path, heated area and rate at which energy reaches the packaging. Different widths, thicknesses and jaw shapes change the thermal mass and contact conditions, even where the same controller is used. The equipment developer must match the band and support materials to a film’s seal layer, expected product dimensions and the repeated heating and cooling stresses of the machine cycle.
Jaw alignment determines whether the heating band contacts the intended seam evenly. If one part of the jaw closes before another, local pressure may be excessive while adjacent regions receive insufficient compression. Wrinkles, product contamination or a displaced pouch can prevent the seal layers bonding even when the controller holds its selected resistance. PackworldUSA’s machines consequently combine electrical control with defined mechanical force, timing and cooling arrangements; selecting a precise setpoint cannot compensate for a defective sealing surface.
The PIREG control range includes DIN rail and panel-mounted units, with industrial communication options for connection to a line controller. The C2-200 uses analogue controls, while the C2-210 and C2-220 support PROFINET and EtherNet/IP respectively. A PIREG-548 touchscreen interface can display operating values and assist with parameter adjustment. These interfaces support recipe management and repeatable settings, but their availability does not establish that an entire packaging process has been validated for a particular product.
Medical sterile barrier packaging requires evidence that the chosen seal process consistently achieves its specified result. Process development establishes a working window for temperature, dwell, pressure and cooling; qualification then tests that window and the equipment’s behaviour in actual use. PackworldUSA offers sealers designed for validation workflows associated with ISO 11607, but equipment capability is distinct from demonstrating compliant seals on a customer’s material and package design. Test methods and acceptance limits still need to be selected and documented.
Changing the packaging material may alter that operating window. A mono-material film introduced to support recycling can soften or crystallise differently from a laminate with a separate sealant layer. Seal initiation temperature, contamination tolerance, strength and package barrier requirements may all change. Resistance feedback can hold the band at a programmed condition, while trials must establish whether the new film forms an acceptable bond under the available sealing pressure and cycle time.
Impulse heating avoids continuously energising the sealing element between cycles, but the difference in electricity consumption depends on the alternative equipment, the number of seals, heating-band dimensions and idle power. PackworldUSA has promoted the approach as energy efficient without publishing a new, independently measured, like-for-like comparison in the 19 October article. Claims of lower scrap likewise require production evidence showing fewer rejected seals under comparable conditions. Precision control supplies one means of limiting variation rather than a guaranteed saving.
PackworldUSA manufactures and integrates precision sealers, while TOSS supplies the resistance-control components and heated bands used in those machines and other industrial systems. Their established approach couples feedback from the electrical heating element with controlled jaw motion and a defined cooling period. The critical qualification task remains to demonstrate that these variables produce acceptable seams throughout a production run, including after material changes, maintenance and adjustments to the machine’s operating speed.